
1-805-484-2992
Quotes - Engineering - SalesMix is a different fluid at each end of the frame
Sugar, stabilizer and solids
A typical mix carries 10–16 percent milkfat, 9–12 percent milk solids-not-fat, 12–16 percent sweetener and a fraction of a percent of stabilizer and emulsifier, for roughly 36–42 percent total solids. Hot, it pumps reasonably well. Below about 60°F the stabilizers start building body, and by aging-tank temperature the mix can be many times thicker than it was at the heater.
The legal hold rises too. Mix pasteurizes at 175°F for 25 seconds, or 180°F for 15 seconds, against 161°F for plain milk. Most HTST mix lines homogenize hot, upstream of the holding tube, so the frame runs as regenerator, heater, out to the homogenizer and hold, back through the regenerator and on into the coolers. Two-stage homogenizing at that temperature builds the fat structure the freezer depends on; the exchanger's part is to deliver mix at a steady temperature without baking sugar and protein onto the heater plates.
Put those together, high temperature on the way up and heavy body on the way down, and the usual answer is a wide-gap plate pack whose cooling sections are often the larger part of the frame.
See the Wide-Gap Plate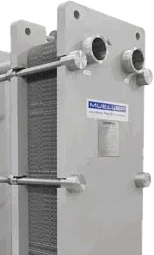
Mix pasteurizing figures
Values a mix frame is usually designed around. Your recipe sheet and utility temperatures replace them at sizing.
| Condition | Typical value |
| HTST hold | 175°F for 25 seconds, or 180°F for 15 seconds |
| Batch alternative | 155°F for 30 minutes in a vat |
| Total solids | About 36–42% |
| Milkfat | 10–16% in most recipes |
| Homogenizer position | Usually hot, upstream of the holding tube |
| Outlet to the aging tank | 36–40°F |
| Plate channel | 6–12 mm wide-gap |
| Cooling utility | Chilled water first, then propylene glycol at a 5–8°F approach |
| Gaskets | NBR or HNBR on product, EPDM on water circuits |
Laying out a mix pasteurizer
How much regeneration a mix frame earns
Mix-to-mix regeneration saves heat just as it does on milk, but wide channels move less heat per plate, so plants commonly settle near 80 percent on mix rather than the 90 percent they run on milk. The PMO rule holding the pasteurized side 1 psi above the raw side applies all the same. The full sequence from blending tank to freezer, including where flavors go in, is set out on our ice cream mix process page; this page stays with the exchanger.
Cooling for the aging tank
Mix leaves the regenerator still warm and should reach aging temperature quickly, both to stop growth and to start the fat crystallizing that aging completes over the next several hours. Plants usually cool in two steps: a chilled-water section that removes most of the heat, then a glycol section that takes the last few degrees.
- Size glycol for the thickest recipe on the schedule
- Expect higher pressure drop on chocolate and high-solids bases
- Keep glycol supply warm enough not to freeze mix on the plate
Chocolate, inclusions and where plates stop
Cocoa adds solids and body, so chocolate mix sets the size of the cooling section on a line that runs both flavors. Nuts, fruit and cookie pieces go in at the freezer, not the pasteurizer, so the mix itself rarely needs a piece-handling tube. Where a fruit base or variegate is heat-treated on its own, it belongs on a single-tube unit.
Burn-on at the heater
Sugar and whey protein together foul a hot wall faster than milk does. Holding the heater approach to 2–5°F over the pasteurizing point keeps the wall temperature down, and the run length between cleanings follows directly from that choice.
Ice cream mix questions
Usually, since both are frozen-dessert mixes held to the same 175°F for 25 seconds or 180°F for 15. Frozen yogurt base is cultured after pasteurizing, so the exchanger only ever sees sweet mix. Soft-serve mix often runs lower in fat and pumps more easily. We size the frame to the thickest recipe on your schedule and check the lightest one against it.
Fat and stabilizer lay down a film on the cold plates, and as it builds, both heat transfer and flow fall away. A cooler sized with no fouling allowance shows it within hours. A wider gap, a sensible margin on area and a glycol supply that is not run too cold all stretch the run before outlet temperature drifts above target.
Most HTST mix lines homogenize hot and upstream of the holding tube, and in many systems the homogenizer also serves as the timing pump. Some plants place it downstream instead. Either way it fixes two pressures the exchanger must respect, the suction it wants and the pressure leaving it, so we need both to size the sections on either side.
Yes, at 155°F for 30 minutes. The exchanger question then becomes cooling only, taking each batch from the vat to aging temperature fast enough to keep the schedule. A small wide-gap or tubular cooler does that well, and it is a common addition when a plant outgrows cooling mix in the vat jacket.
Mix fat is lower than heavy cream, but it is enough to shorten EPDM life on the product side over a season of daily runs. Most mix frames go to nitrile or HNBR on product and keep EPDM on the water circuits. Tell us your cleaning chemistry and peak temperature and we match the compound to both.
Related
Dairy Solutions
Cream Heating
A cream heat exchanger sized for heavy cream: wide-gap plates above about 30 percent fat, 166°F pasteurizing and cooling that protects the fat.
+ Learn More
Dairy Solutions
Butter Cream
Butter cream ripening starts in the heat exchanger: pasteurize hot, then cool to the temperature that sets butterfat crystals before the churn.
+ Learn More
Dairy Solutions
Cream & Ice Cream Mix
Cream heat exchanger and ice cream mix exchanger selection: when fat and viscosity move a dairy duty from standard plates to wide-gap or tubular.
+ Learn More
