
1-805-484-2992
Quotes - Engineering - SalesWhy heavy cream outgrows a milk plate
Viscosity, not heat load, sets the pack
Measured by heat load, cream is an easy duty: its specific heat is lower than milk's and plant cream flows are usually modest. The trouble is hydraulic. At 166°F, 40 percent cream still moves through a standard plate without much trouble. Cool it toward 40°F and its viscosity climbs many times over, so the same 3–5 mm channel that served the heater now chokes the cooler. The symptoms are familiar to anyone who has tried it: a timing pump that cannot hold rate, a cooling section that needs far more pump head than the drawings show, and gaskets lifting out of their grooves at the outlet end.
Wide-gap plates open the channel to about 6–12 mm. Velocity falls, the film coefficient falls with it and the pack gets longer, but pressure drop comes back within what a booster and a timing pump can deliver. Lower shear also matters to the product. Cream forced through narrow, fast channels loses fat globule membrane, and the plant sees the damage later as poor whipping, cream plug in the bottle neck or free fat in the finished product.
Where cream above 30 percent is only part of the schedule, one frame can carry wide-gap plates in its cooling section and standard plates in the heater. We size each section on its own numbers.
See the Wide-Gap Plate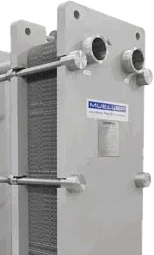
Cream heating duty at a glance
Typical design values for a heavy-cream pasteurizer. Your own fat, flow and utility temperatures replace them when we size the unit.
| Condition | Typical value |
| Pasteurizing temperature and hold | 166°F for 15 seconds minimum; 150°F for 30 minutes in a vat |
| Fat range where wide-gap is used | Above about 30%; heavy cream 36–40% |
| Channel gap | 6–12 mm wide-gap; 3–5 mm standard below 30% fat |
| Cooled outlet | 45°F or below; most plants target 36–40°F |
| Heater approach on hot water | 2–5°F above pasteurizing temperature at the outlet |
| Cooler approach | 2–4°F on chilled water, 5–8°F on propylene glycol |
| Gaskets | NBR on product, EPDM on water, FDA 21 CFR 177.2600 compounds |
| Product-side build | 316L, tri-clamp, drainable, 32 Ra (20 Ra on request) |
| Sanitary standard | 3-A 11-10 where the inspector expects the symbol |
Getting cream through the pasteurizer intact
Regeneration on a cream unit
Cream-to-cream regeneration follows the same PMO rule as milk: the pasteurized side runs at least 1 psi above the raw side, so a pinhole leaks the safe way. Viscous cream loses pressure faster along its path, so the margin is thinnest at the cold end of the regenerator, where pasteurized cream leaves and raw cream enters. We check the differential there, on a pack fouled toward the end of a run, not only on a clean one. The general layout is covered under HTST and regeneration.
Holding the fat together
Every pump, valve and narrow passage between the separator and the filler is a chance to break fat globules. Inside the exchanger the control is velocity: open channels, sensible pass arrangements and no throttling at the cooler outlet to build back-pressure.
- Size the gap for the coldest outlet you will ever run
- Avoid valves that throttle cold cream to make pressure
- Check pump speed against the whipping test, not only flow
- Keep cooler passes short where fat damage has been seen before
When tubes are the better answer
Cream above about 45 percent fat, cream carrying cocoa or flavor solids, and cream heated far above HTST for extended shelf life all lean toward tubes. A multi-tube unit takes higher pressure and has no gaskets in the product path, at the cost of wider approaches and more floor length.
What to send for a cream quote
The fastest cream quotes arrive with these filled in.
- Fat percent of every cream the line runs
- Flow in lb/h or gal/h, and hours per run
- Raw inlet, pasteurizing and final outlet temperatures
- Hot water and chilled water or glycol temperatures
- Regeneration wanted, and complete unit or plate pack only
Before you size for cream
It is the legal HTST minimum for products of 10 percent fat or more, held 15 seconds, and many plants run a few degrees above it for margin. Cream labeled ultra-pasteurized is a diffrent duty: 280°F or above for at least 2 seconds. That unit is a tubular or shell-and-tube design, not a wide-gap plate pack.
It depends on the fat and the cold outlet, so we do not quote a fixed ratio. Lower velocity means less heat moved per plate, so more area is needed for the same approach. What you buy with that area is runs that do not stall and gaskets that stay seated. When cream sits near 30 percent fat we size both options for comparison.
Yes, if glycol is the only cold utility in the plant. Expect a 5–8°F approach and a longer cooling section than chilled water would need. Watch the glycol supply temperature: glycol fed well below the freezing point of cream can freeze a film on the plate and push pressure drop up sharply. We set a minimum supply temperature with the sizing.
A cream HTST also needs a holding tube sized for 15 seconds at the cream flow, a flow-diversion valve, a timing pump and recording controls. We size and build the exchanger and hand over the outlet temperatures and pressure profile those parts must work with, so whoever supplies the hold and the valve can match them to the heater.
Related
Dairy Solutions
Ice Cream Mix
An ice cream mix pasteurizer heats mix to 175°F for 25 seconds, then cools it for the aging tank. How sugar, stabilizer and solids shape the exchanger.
+ Learn More
Dairy Solutions
Butter Cream
Butter cream ripening starts in the heat exchanger: pasteurize hot, then cool to the temperature that sets butterfat crystals before the churn.
+ Learn More
Dairy Solutions
Cream & Ice Cream Mix
Cream heat exchanger and ice cream mix exchanger selection: when fat and viscosity move a dairy duty from standard plates to wide-gap or tubular.
+ Learn More
